PCB Assembly
Zhang

 NextPCB Capabilities
Printed Circuit Boards
 Process Capabilities
 PCB Design-Aid & Layout
 Quality
 Drills & Throughplating
 Factory & Certificate
 PCB Assembly Factory Show
Certificate

Support Team
Feedback:
support@nextpcb.com


A guide to PCB and PCBA test methods: principles, pros and cons, standards, and deployment
Introduction: This page organizes PCB/PCBA quality verification by test category. For each category you’ll find the method, how it works, core benefits and trade-offs, typical use cases, and commonly referenced standards. Use it to design a right-sized test strategy from prototype to mass production.
NextPCB supports SPI, AOI, X-ray inspection, ICT (flying probe or bed-of-nails), and FCT, plus ionic contamination and reliability testing (such as thermal shock and microsection), as part of its quality flow. Upload your files and get a fast, engineer-reviewed quote.
Upload Gerber/ODB++ Get Instant Quote
Definition: PCB testing is the staged verification of bare boards and assembled PCBAs to prove design intent, electrical safety, and long-term reliability from prototype through mass production. It’s not one tool but a layered stack you right-size for risk, volume, and budget—catching issues as early (and cheaply) as possible while maintaining diagnostic depth.
PCB testing vs. PCBA testing: PCB (bare-board) testing checks the unpopulated board before assembly—electrical opens and shorts, dimensions, plating, and material reliability. PCBA testing checks the assembled board—solder and placement quality, electrical connectivity, and functional behavior. Most quality plans use both.
At a glance, the stack:
Use this guide to choose the minimum-viable set that balances coverage, diagnostic power, cycle time, and fixture cost for your design.
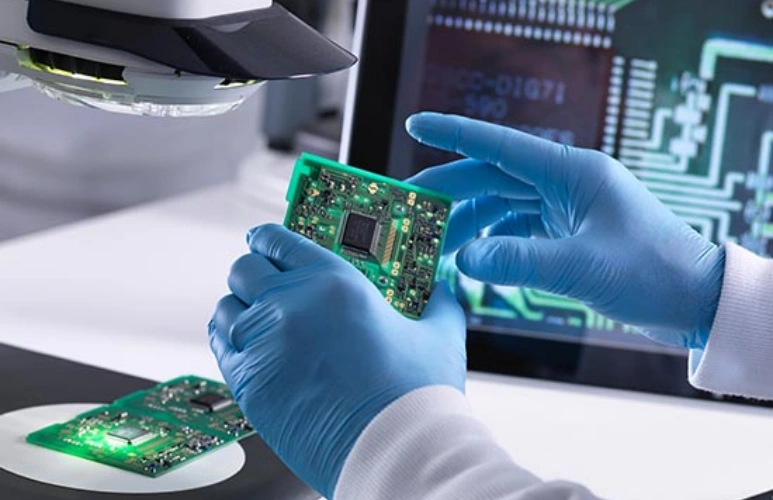
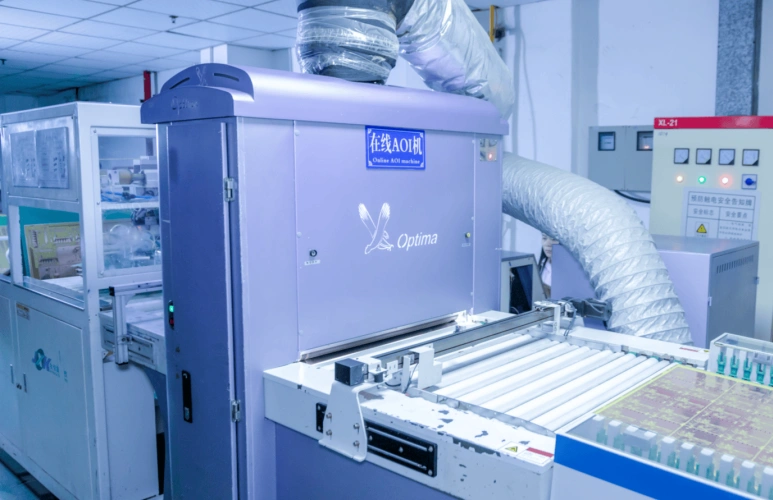
Optical inspection looks for visible defects before they become electrical failures. It ranges from manual checks with a loupe to automated optical inspection (AOI) that compares camera images to a golden reference. Modern 3D AOI also measures height/volume, so it can spot tombstoning, polarity errors, and insufficient solder more reliably than 2D. It’s fast, non-contact, and ideal for early, high-throughput screening.
| Method | How it works | Strengths | Limitations | Typical use / Standards |
|---|---|---|---|---|
| Manual visual inspection | Human inspection with magnifier or microscope | Lowest cost; flexible for rework triage | Throughput and consistency vary with operator | Prototypes, repair screening |
| 2D AOI | Camera image plus grayscale/color/template comparison | Fast, easy to deploy | Height/occlusion sensitivity; false calls on silk or glare | Low–mid complexity SMT screening |
| 3D AOI | Structured light/Moiré height map; reconstructs joint and component geometry | Quantifies height/volume; robust on tombstoning, polarity, misorientation; great with SPI data | Higher capex; tuning required | Primary station for mid/high-density SMT lines (acceptance per IPC-A-610) |
Takeaway: 3D AOI is becoming mainstream; pairing SPI → AOI creates a closed loop to stop defects early.
Many SMT defects start at the stencil printer, so SPI measures the volume, height, area, and offset of solder paste on each pad. By catching underprint, bridging risk, or misalignment before placement, SPI prevents expensive downstream rework. The data also feeds process control (SPC), helping tune printer parameters and stencil designs. For fine-pitch parts (0201, BGA/QFN), SPI is a must-have gate.
| Method | How it works | Strengths | Limitations | Typical use / Standards |
|---|---|---|---|---|
| 3D SPI | Structured light or laser scan of volume/height/area/offset on pads | “Gate #1” before reflow; strong predictors for bridges and insufficient paste; data-driven SPC | Needs stable optics/fixtures and calibration | Essential for 0201, BGA/QFN, fine-pitch SMT (print requirements per IPC-7527) |
Electrical tests prove that the board isn’t just pretty—it actually works. Bare-board E-test checks fabricated boards for opens and shorts before assembly. For assembled boards, Flying Probe is fixture-less and flexible for prototypes, while ICT uses a bed-of-nails for fast, parallel coverage in mass production. Boundary scan (JTAG) reaches dense or hidden nets without probes, and FCT powers the board in realistic conditions to catch system-level issues. Together they balance coverage, speed, and cost across the product lifecycle.
| Method | How it works | Strengths | Limitations | Typical use / Standards |
|---|---|---|---|---|
| Bare-board E-test (BBT) | Flying-probe or fixture-based electrical test of the unpopulated PCB; every net is checked for opens and shorts against the netlist | Catches fabrication defects before assembly adds cost | Does not test assembled components or function | Standard release test for fabricated boards (IPC-9252) |
| Flying Probe (FPT) | Moving probes test nets parameter by parameter | No fixture; great for frequent ECOs | Slower than ICT | Small lots, many SKUs, complex boards |
| In-Circuit Test (ICT) | Bed-of-nails fixture tests nets and components in parallel | Broad coverage; fast and precise fault isolation | Fixture cost and lead time | Mass production workhorse |
| Functional Test (FCT) | Powers the board in a system-like environment | Closest to real use; catches interaction issues | Custom fixtures and firmware needed | Final release, system validation (see a sample test report) |
| Boundary Scan (JTAG / IEEE 1149.1) | Scan chain tests interconnects among scan-capable ICs | Fixture-less access to dense/hidden nodes; complements ICT | Requires scan-enabled devices and test vectors | High-density digital boards; mixed strategy with ICT |
Takeaway: Use ICT for volume, Flying Probe for prototypes and frequent ECOs, and FCT as the final release gate. See ICT vs FCT for the coverage matrix and the PCBA testing methods guide to choose by build stage. Need FCT on your own build? See our PCBA functional testing service; free functional testing is available for up to 5 boards on qualifying orders.
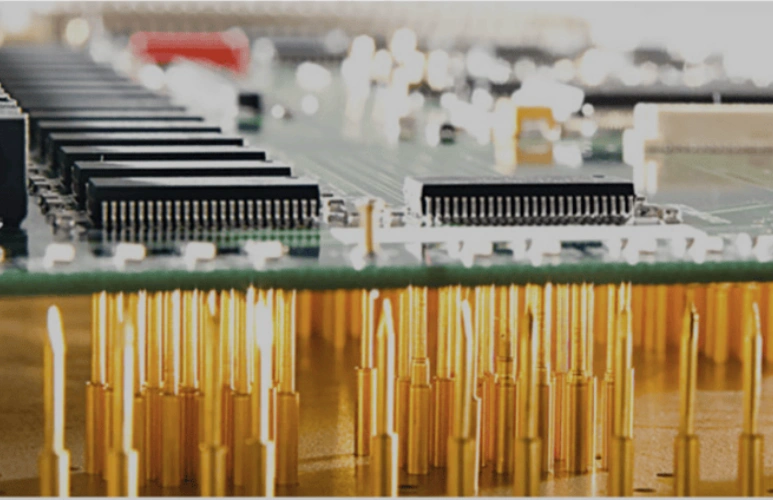
Some faults hide inside the board or under components. AXI X-ray reveals voids and bridges in hidden joints like BGA, while C-SAM ultrasound detects delamination and voids in laminates and packages. When root cause demands it, microsectioning cuts and polishes a small coupon to show vias, copper thickness, and resin flow directly. NDT preserves the product; destructive analysis delivers the most detail.
| Method | How it works | Strengths | Limitations | Typical use / Standards |
|---|---|---|---|---|
| AXI (2D/3D/CT X-ray) | X-ray transmission; 3D/CT reconstructs joint volumes and voiding | Only reliable view into hidden joints (BGA/QFN); quantifies void %, bridges, insufficient solder | Higher cost; CT throughput trade-offs | Automotive/medical/aerospace; BGA/QFN; through-hole reflow fill (IPC-A-610, IPC-7095) |
| SAM / C-SAM (acoustic microscope) | High-frequency ultrasound echo imaging through layers | Non-destructive detection of delamination, voids, air gaps | Limited on thick metal stacks | Lamination quality; package–board composites |
| Microsection (destructive cross-section) | Sample, mount, grind/polish; microscope analysis | Direct view of via copper, resin flow, layer registration, inter-laminar issues | Destructive; cycle time | Process validation and failure analysis (IPC-TM-650 family) |
Surface finishes (ENIG, ENEPIG, etc.) and plating quality drive both reliability and appearance. XRF quickly and non-destructively measures coating thickness and alloy ratios to verify process control. Solderability tests quantify how well pads wet with a given alloy, especially after storage or finish changes. These checks reduce risks like black pad, poor wetting, and early field failures.
> HASL vs ENIG: An Ultimate Guide on Surface Finish
| Method | How it works | Strengths | Limitations | Typical use / Standards |
|---|---|---|---|---|
| XRF thickness/composition | X-ray fluorescence quantifies plating thickness and alloy ratios | Fast, non-destructive, traceable | Very thick or non-metal stacks may need microsection | ENIG/ENEPIG, gold fingers incoming/outgoing (e.g., ASTM B568) |
| Solderability testing | Wetting balance; edge dip / steam aging then wetting force vs time | Quantifies wetting across finishes and solders | Strict specimen prep and aging needed | Finish changes; long-storage releases (e.g., J-STD-003) |
Flux residues and trapped ions can trigger electrochemical migration, corrosion, or leakage over time. ROSE gives a fast read on total ionic residues for day-to-day process monitoring, while ion chromatography identifies the exact contaminants during investigations. Cleanliness matters most for high-impedance, high-reliability, or harsh-environment products. Keeping residues in control extends lifetime and reduces intermittent field issues.
| Method | How it works | Strengths | Limitations | Typical use / Standards |
|---|---|---|---|---|
| ROSE | Solvent extract conductivity → NaCl equivalent (total residues) | Simple, fast, SPC-friendly | Total only—no speciation | Routine flux/cleaning process control (IPC-TM-650 2.3.25) |
| Ion Chromatography (IC) | Separates and quantifies anions/cations/weak organic acids | High diagnostic power; traceable | More complex workflow and time | Failure analysis; customer compliance reports (IPC-TM-650 2.3.28) |
Reliability tests accelerate real-world stresses to expose long-term risks. SIR evaluates insulation behavior under heat, humidity, and bias; CAF checks whether conductive filaments may form within the laminate; thermal cycling/shock probes solder and interlayer fatigue. These methods validate new materials and processes, and they’re standard for automotive, medical, and aerospace. The goal is predictable lifetime, not just day-one pass.
| Method | How it works | Strengths | Limitations | Typical use / Standards |
|---|---|---|---|---|
| SIR | Monitors surface insulation resistance under temperature, humidity, and bias | Evaluates ECM risk and flux/cleaning compatibility | Long test durations | Flux/cleaning validation (IPC-TM-650 2.6.3.7; with J-STD-004) |
| CAF | Assesses conductive anodic filament formation between glass bundles | Material/process compatibility indicator | Test coupons and time cost | HDI/long-life/high-reliability designs (IPC-TM-650 2.6.25) |
| Thermal cycling/shock | Temperature stress on solder joints and interlayers | Approximates field conditions | Requires dedicated chambers | Automotive, aerospace, outdoor equipment (e.g., JESD22) |
As data rates climb, signal integrity becomes as critical as connectivity. TDR confirms controlled impedance and finds discontinuities, while insertion-loss/S-parameters quantify frequency-domain losses and de-embedding-ready behavior for 10+ Gbps links. For power and medical designs, HiPot/IR verifies dielectric isolation to meet safety regulations. These tests ensure both fast signals and safe operation.
| Method | How it works | Strengths | Limitations | Typical use / Standards |
|---|---|---|---|---|
| TDR impedance | Time-domain reflectometry for characteristic impedance and discontinuities | Factory must-have for controlled impedance; locates defects | Does not quantify high-frequency loss | Controlled-impedance boards, backdrill, differential pairs (IPC-TM-650 2.5.5.7) |
| Insertion loss / S-parameters | Frequency-domain loss including copper roughness and dielectric contributions | Suited for ≥10 Gbps links | Demands accurate fixtures and de-embedding | Backplanes, server boards, cable assemblies (IPC-TM-650 2.5.5.12a) |
| HiPot / IR / HV-MIR | Dielectric withstand and insulation resistance under high voltage | Ensures isolation and safety compliance | High-voltage safety and fixtures required | Power, medical, industrial isolation (IPC-TM-650 2.5.7 family) |
Mechanical accuracy underpins assembly yield. Non-contact profilometry verifies outline, hole sizes, and flatness; warpage under reflow predicts opens or cracks in large-array packages like BGAs. Coplanarity and local stiffness also affect print quality and solder joint geometry. By measuring geometry at room temperature and through the thermal profile, you prevent latent defects before they reach the customer.
| Method | How it works | Strengths | Limitations | Typical use / Standards |
|---|---|---|---|---|
| Laser/white-light interferometry | Non-contact 3D profilometry of outline, holes, and planarity | Fast, precise | Needs appropriate surface reflectance | Dimensional QC, flatness SPC |
| Reflow-condition warpage | Real-time board/region warpage under reflow profile | Strong predictor of BGA cracking and open joints | Tooling and fixturing requirements | Large-array packages; design/process optimization (IPC-9641 guidance) |
This part helps to translate the categories above into practical, right-sized test flows you can run on the line. Each playbook balances coverage, cost, and speed, and can be scaled up or down by risk.
3D SPI → 3D AOI → targeted AXI (critical parts) → (as needed) Flying Probe / FCT → TDR for controlled-Z → ROSE/IC sampling
3D SPI and 3D AOI throughout → ICT as primary electrical test → targeted AXI on BGA/QFN → HiPot/IR where safety isolation applies → XRF and solderability sampling
Add SIR/CAF, C-SAM, reflow warpage monitoring, periodic microsection. For high-speed links include insertion loss/S-parameters. Verify product-level conformance (e.g., IPC-6012 for via reliability, backdrill, cavities).
Prototype batches, fast ECOs, high-reliability builds—tell us your priorities and we will propose the right test stack for your build: SPI and AOI gates, X-ray sampling, ICT or flying probe, FCT, and cleanliness and reliability tests where your product needs them.
Start a Prototype Run PCB Capabilities PCBA Capabilities
PCB testing checks the bare board before assembly: opens and shorts, dimensions, plating, and material reliability. PCBA testing checks the assembled board: solder and placement quality, electrical connectivity, and functional behavior. Most quality plans use both.
The main categories are optical inspection (AOI), solder paste inspection (SPI), electrical and functional test (flying probe, ICT, boundary scan, FCT), internal structure analysis (X-ray, C-SAM, microsection), surface finish and solderability, cleanliness, reliability and environmental stress, high-speed and dielectric/safety tests, and mechanical or warpage measurements. Sections 1–9 describe each.
There is no single test. A typical flow is bare-board electrical test, then SPI, AOI, X-ray on hidden joints (BGA/QFN), ICT or flying probe, and finally FCT, with cleanliness and reliability tests sampled as the product requires. The PCBA testing methods guide shows how to choose by build stage.
Bare-board testing is the electrical test of the unpopulated PCB. Flying-probe or fixture-based testers check every net for opens and shorts against the netlist before the board goes to assembly. IPC-9252 gives guidelines for it.
AOI handles visible features and solder fillets; AXI is required for hidden joints and internal defects. They are complementary.
Use Flying Probe for prototypes and rapid changes; ICT for high-volume, fast parallel coverage and precise isolation.
ROSE gives total ionic residue for process control; Ion Chromatography identifies which ions and supports root-cause analysis and customer reporting.
XRF is fast and non-destructive for routine release; microsection is destructive but reveals full stack details—best for validation and failure analysis.
On new materials/processes, high-reliability products, and periodically for surveillance.
| Domain | Methods | Example standards/guides |
|---|---|---|
| Optical/visual | 3D AOI | IPC-A-610 (acceptability); vendor specs; internal limits |
| Paste/print | 3D SPI | IPC-7527; vendor application notes; internal process specs |
| Electrical/functional | Bare-board E-test, FPT, ICT, FCT, JTAG | IPC-9252 (bare-board electrical test); IEEE 1149.1 (boundary scan) |
| X-ray | AXI (2D/3D/CT) | IPC-A-610; IPC-7095 (BGA); vendor methods; internal acceptance criteria |
| Acoustic | C-SAM | Vendor methods |
| Plating/solderability | XRF; Solderability | ASTM B568; J-STD-003 |
| Cleanliness | ROSE; IC | IPC-TM-650 2.3.25 / 2.3.28 |
| Reliability | SIR; CAF; Thermal cycling | IPC-TM-650 2.6.3.7 / 2.6.25; JESD22 |
| High-speed/dielectric | TDR; S-parameters | IPC-TM-650 2.5.5.7 / 2.5.5.12a |
| Safety | HiPot/IR | IPC-TM-650 2.5.7 family; safety regulations |
| Warpage | Reflow warpage | IPC-9641 guidance |
Upload your design and tell us your priorities (speed, coverage, cost). NextPCB will propose a phased test strategy and deliverables you can approve in one go. Already have a test plan? See our PCBA functional testing service.
Upload & Quote Engineer Consultation
A layered strategy—SPI → AOI → AXI/E-test → reliability/cleanliness → final release—is the modern best practice for PCB/PCBA quality. Tailor your stack to product traits (high-speed, safety, lifetime) and to build phase (prototype vs. volume). The category-by-category map above helps you choose the minimum viable yet risk-appropriate test set while keeping cost and throughput under control. To go deeper, read 13 Popular PCB Test Methods in PCB Manufacturing.
Still, need help? Contact Us: support@nextpcb.com
Need a PCB or PCBA quote? Quote now