Julia Wu - Senior Sales Engineer at NextPCB.com

 NextPCB Capabilities
Printed Circuit Boards
 PCB Assembly
 Layer Buildup
 SMD-Stencils
 PCB Design-Aid & Layout
 Mechanics
 Quality
 Drills & Throughplating
 Factory & Certificate
 PCB Assembly Factory Show
Certificate

Support Team
Feedback:
support@nextpcb.com


HASL vs lead-free HASL is a choice between two versions of the same finish. Hot air solder leveling (HASL) coats the exposed copper pads of a PCB with molten solder and levels it with hot air knives. HASL with lead uses a tin–lead (Sn–Pb) alloy. Lead-free HASL (also written lead-free HASL, leadfree HASL or LF-HASL) uses a tin-based alloy with no added lead, such as tin–silver–copper (SAC) or tin–copper. The process is the same. The differences are the alloy, the process temperature, RoHS compliance, appearance and how the board handles thermal stress.
This guide compares the two side by side and explains how lead-free HASL is applied, where each one fits, and when to pick a flatter finish instead. For the full range of options, see the PCB surface finish guide or the surface finish options NextPCB supports.
| Attribute | HASL (with lead) | Lead-free HASL |
|---|---|---|
| Solder alloy | Tin–lead, commonly Sn63/Pb37 | Lead-free tin alloy, such as SAC (tin–silver–copper), tin–copper or tin–copper–nickel |
| Alloy melting point | 183 °C (eutectic Sn63/Pb37) | About 217–227 °C, depending on the alloy |
| Process temperature | Lower | Higher, typically 260–270 °C at the solder pot |
| RoHS compliant | No | Yes |
| Appearance | Bright and shiny | Duller, slightly grainy |
| Wetting and solderability | Excellent | Excellent, but needs a tighter process window |
| Thermal stress on the board | Lower | Higher |
| Surface flatness | Uneven; thicker on large pads | Uneven; thicker on large pads |
| Fine-pitch and BGA suitability | Poor | Poor |
| Cost | Lowest of the common finishes | Low; usually slightly above leaded HASL |
| Best for | Low-cost boards where lead-free is not required | RoHS-compliant, general-purpose boards with through-hole parts and larger SMD pads |
In short, choose lead-free HASL whenever the board must be RoHS-compliant. Both versions share the same weakness: an uneven surface that is a poor fit for fine-pitch parts. If your design has those, compare them with ENIG or OSP.
HASL with lead is the original form of hot air solder leveling. The board is fluxed, dipped in a pot of molten tin–lead solder, and withdrawn between hot air knives that blow off the excess and level the coating. The eutectic Sn63/Pb37 alloy melts at a single temperature, 183 °C, which gives good wetting and a bright finish. For more on the process itself, read the detailed explanation of hot air solder leveling.
| Advantages | Disadvantages |
|---|---|
|
|
Lead-free HASL (LF-HASL) is the same process run with a lead-free solder alloy. The alloy is mostly tin, with small additions of silver and copper (SAC), copper alone, or copper with nickel. These alloys melt at higher temperatures than Sn–Pb, so the pot and the air knives run hotter. The result is a RoHS-compliant coating with the same low cost and long shelf life as leaded HASL. To compare the alloys themselves, see lead vs lead-free solder and the melting point of solder.
| Advantages | Disadvantages |
|---|---|
|
|
| Step | What happens |
|---|---|
| 1. Micro-etch and clean | The copper pads are cleaned and lightly etched so the solder wets evenly. |
| 2. Flux | A flux coating is applied to the board so the molten solder wets the copper. |
| 3. Solder dip | The board is dipped in a pot of molten lead-free solder, typically at 260–270 °C. |
| 4. Hot air leveling | Hot air knives blow excess solder from the pads and plated holes, leaving a thin, levelled coating. |
| 5. Cooling | The solder solidifies on the pads. |
| 6. Wash | The board is washed to remove solder flux residue and dried. |
Because the molten solder and air knives are hotter than in leaded HASL, the base material must tolerate more thermal shock. Pad thickness still varies with pad size: large pads end up with thicker solder than small pads, which is why HASL is not recommended for fine-pitch components.
The EU RoHS Directive took effect on 1 July 2006 and limits lead to 0.1% by weight in each homogeneous material. A tin–lead HASL coating is far above that limit, so leaded HASL is not RoHS-compliant. Lead-free HASL, ENIG, OSP, immersion silver, immersion tin and ENEPIG are all lead-free options. If your product ships to the EU or any market with similar rules, or your customer specifies RoHS, use lead-free HASL or another lead-free finish. For the full list of lead-free finishes, see the PCB surface finish guide.
| Board or design | Lead-free HASL | Why |
|---|---|---|
| Double-sided boards | Suitable | Plated through-holes and larger pads take the finish well. |
| Multilayer boards | Suitable, with limits | The higher process temperature adds thermal stress, so confirm the material and stack-up with your manufacturer. |
| Through-hole and large SMD designs | Suitable | Wide pads and spacing tolerate the uneven surface. |
| Fine-pitch SMT and BGA (about 0.5 mm pitch and finer) | Not recommended | Uneven solder thickness and bridging risk; use ENIG or OSP. |
| HDI boards | Not recommended | Fine features need a flat surface. See HDI PCB manufacturing. |
| Gold fingers and contacts | Not suitable | Contacts need hard gold. See the gold fingers guide. |
| Low-cost base materials such as CEM-1 | Check first | The finish goes on copper and does not depend on the base material, but the board must survive the solder bath. Confirm the material and finish combination with your manufacturer. |
| If your board... | Choose |
|---|---|
| Must be RoHS-compliant and uses larger parts | Lead-free HASL |
| Has no lead restriction and cost is the only driver | HASL with lead |
| Has fine-pitch parts or BGA | ENIG (flat, long shelf life) |
| Needs a flat pad at the lowest cost and will be assembled quickly | OSP |
| Has edge connectors that are plugged in repeatedly | Hard gold (gold fingers) |
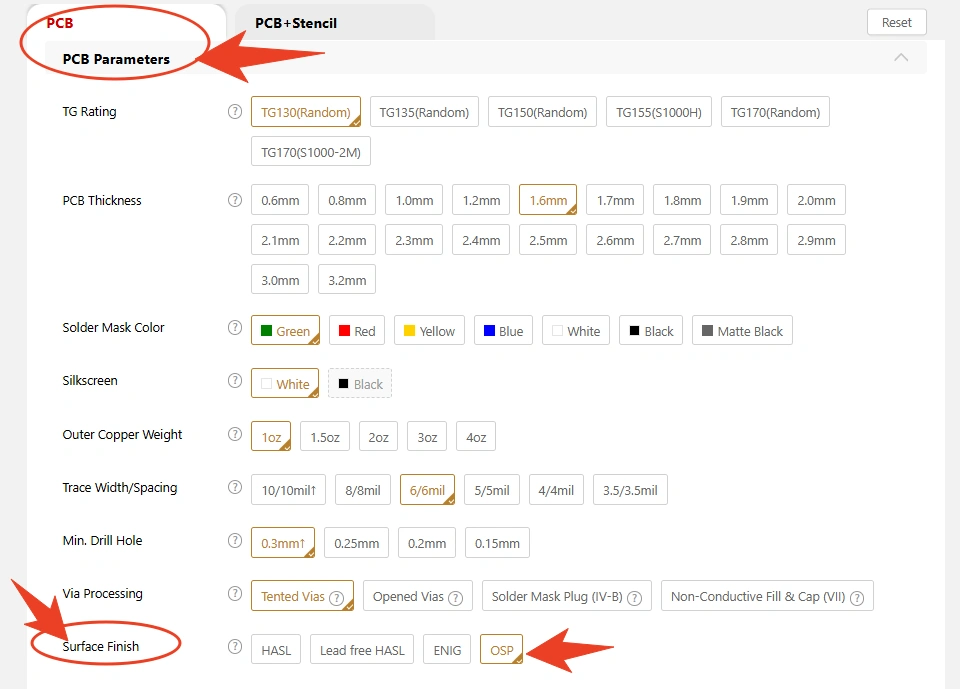
NextPCB offers both HASL and lead-free HASL in the standard PCB quote, alongside ENIG and OSP. HASL is the default option in the quote form, so check the surface finish field and select Lead-Free HASL if your board must be RoHS-compliant. Immersion silver, immersion tin, ENEPIG and hard gold are available through the advanced PCB quote. See PCB capabilities for specifications, or compare every option on the PCB surface finish options page.
HASL with lead uses a tin–lead solder alloy (commonly Sn63/Pb37), while lead-free HASL uses a tin-based alloy with no added lead, such as SAC or tin–copper. Lead-free HASL runs at a higher temperature, looks duller, and is RoHS-compliant. The process and the uneven surface are otherwise the same.
Not by default. Standard HASL traditionally means tin–lead solder, which is not RoHS-compliant. Lead-free HASL is the version that uses lead-free solder. Always confirm which one is selected on your order.
Yes. Lead-free HASL uses an alloy without added lead, so it meets the RoHS limit of 0.1% lead by weight in homogeneous materials. Leaded HASL does not meet it.
Lead-free alloys solidify differently from eutectic tin–lead and give a duller, slightly grainy surface. The appearance is normal and does not by itself indicate poor solderability.
The solder pot typically runs at about 260–270 °C, higher than for leaded HASL, because lead-free alloys melt at roughly 217–227 °C compared with 183 °C for Sn63/Pb37.
Usually slightly, because of the alloy and the higher process temperature. Both remain among the lowest-cost finishes, well below ENIG, ENEPIG and immersion silver.
Yes. Double-sided boards are a typical use. For multilayer boards the higher process temperature adds thermal stress, so confirm the material and stack-up with your manufacturer.
It is not recommended. HASL leaves an uneven surface and can bridge fine-pitch pads. Use ENIG for fine-pitch parts and BGA, or OSP when boards are assembled promptly.
The finish is applied to the copper, so it does not depend on the base material. The board must still tolerate the thermal shock of the solder bath, which is greater for lead-free HASL. For lower-cost materials such as CEM-1, confirm the material and finish combination with your manufacturer before ordering.
Still, need help? Contact Us: support@nextpcb.com
Need a PCB or PCBA quote? Quote now