NextPCB Capabilities
Printed Circuit Boards
 Process Capabilities
 PCB Design-Aid & Layout
 Quality
 Drills & Throughplating
 Factory & Certificate
 PCB Assembly Factory Show
Certificate

Support Team
Feedback:
support@nextpcb.com


A PCB surface finish (also called a PCB surface treatment or surface plating) is a thin metallic or organic coating applied to the exposed copper pads of a printed circuit board. It protects the copper from oxidation and gives components a solderable surface. The main types are HASL, immersion tin, immersion silver, ENIG, ENEPIG, electroplated nickel/gold (hard and soft gold) and OSP. The right choice depends on component pitch, assembly process, storage time, contact wear, RF performance and cost.
This guide explains how each finish works, compares their strengths and limits in tables, and shows how to choose one for your board. If you already know what you need, see the PCB surface finish options NextPCB supports and where to order each one.
A PCB surface finish is a layer, formed on the component contact areas and electrical connection points of a printed circuit board, that differs from the base material in mechanical, physical and chemical properties. It protects the exposed copper from environmental factors such as oxidation and provides a surface suitable for soldering, so components can be reliably connected to the PCB. It also has to meet requirements for environmental protection, electrical performance, physical strength and durability.
The copper on a circuit board is the base surface for soldering. Without a protective coating, exposed copper oxidizes easily, and the copper oxide layer significantly reduces soldering quality and the reliability of the final product. During soldering, the finish helps form the intermetallic connection between the copper pads and the component leads. It is the outermost layer on top of the copper, acting as a “coating” on the copper.
Surface finishing is one of the most important steps in PCB manufacturing, covering both fabrication and assembly. As shown in the figure below, the finish sits at the outermost layer of the PCB, above the copper layer.
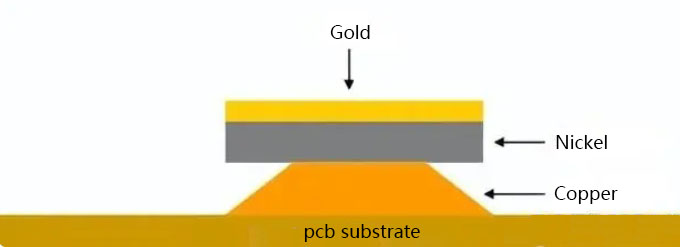
The two jobs of a surface finish:
What happens without one: a thick oxide layer stops molten solder from wetting the copper, which leads to weak or open solder joints, rework and field failures.
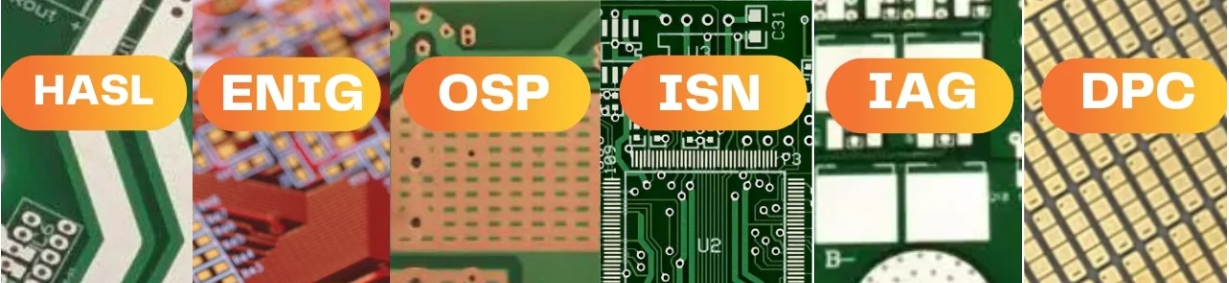
The table compares the finishes covered in this guide. Pros, cons and fit for each one follow below.
| Finish | Lead-free | Pad flatness | Shelf life | Best for | Main limitation |
|---|---|---|---|---|---|
| Leaded HASL (Sn–Pb) | No | Uneven | Long | Low-cost boards where lead-free is not required | Not RoHS-compliant; rough surface |
| Lead-free HASL (SAC) | Yes | Uneven | Long | General-purpose and volume production | Rough surface; not for fine pitch or contacts |
| Immersion tin (chemical tin) | Yes | Excellent | Short (about 6 months) | Fine-pitch SMT, BGA, small components | Tin-whisker risk in storage; sensitive to handling |
| Immersion silver | Yes | Flat | Short | Aluminum wire bonding, EMI shielding, fine lines, membrane switches | Easily contaminated; short assembly window after opening |
| ENIG | Yes | Very flat | Long | Fine-pitch and BGA boards, long storage, multiple reflows | Higher cost; black pad risk; possible RF loss |
| ENEPIG | Yes | Very flat | Long (about 12 months or longer) | Soldering plus wire bonding, high-end packaging | Higher cost; thin soft gold needs protection |
| Electroplated Ni/Au (hard or soft gold) | Yes | Flat | Long | Gold fingers and contacts (hard gold); wire bonding (soft gold) | High cost; complex plating and masking; thick gold is not solderable |
| OSP | Yes | Flat | Short | Cost-sensitive fine-pitch SMT with fast assembly | Short shelf life; limited rework; not for wave soldering |
PCB surface finishing has changed with electronics manufacturing, moving from simple flux protection to flat, lead-free finishes.
| Stage | Finish or process | Why it emerged |
|---|---|---|
| Early boards | Flux applied directly to copper | Simple, but it could not protect the copper for long, and soldering quality depended heavily on the environment |
| Mass production | Electroplated tin–lead (Sn–Pb) | Good solderability and effective protection of the copper layer |
| Solder mask era | Hot air solder leveling (HASL) | Coating copper with solder and leveling it with hot air improved soldering performance and reliability |
| Higher routing density | OSP | Flatter surfaces for fine-pitch components, with low cost and environmental friendliness |
| Clean assembly and long storage | ENIG | Excellent flatness and anti-oxidation capability |
| Lead-free regulation | Lead-free HASL, immersion silver, immersion tin, ENEPIG, ENIAg | Good soldering performance with environmental compliance for high-density, high-performance products |
The EU RoHS Directive (adopted in 2003 and enforced from July 2006) was the watershed. It drove three changes:
Metal-type finishes deposit a metal layer on the copper pads by hot-dip soldering (HASL), chemical displacement (immersion tin and silver), electroless plating (ENIG and ENEPIG) or electroplating (hard and soft gold).
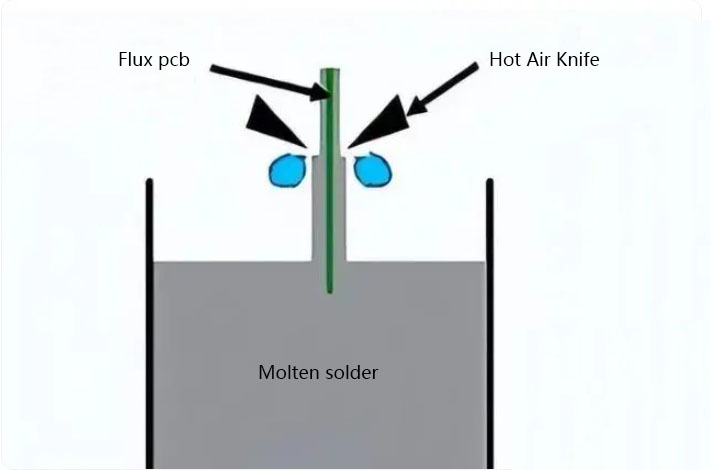
Hot Air Solder Leveling (HASL), also known as tin spraying, immerses the PCB in molten solder to form a solder layer on the copper surface. High-temperature compressed air (air knives) then blows off the excess solder before it solidifies, leaving a flat, uniform surface. During the process, Cu–Sn intermetallic compounds (IMC) form, which improves adhesion and soldering performance. The air knives reduce the meniscus effect and suppress bridging.
| Dimension | Leaded HASL (Sn–Pb) | Lead-free HASL (SAC) |
|---|---|---|
| Melting point | Low (about 183 °C) | High (about 217 °C) |
| Solder joint appearance | Bright, excellent wettability | Higher mechanical strength, environmentally friendly |
| Environmental compliance | Not RoHS-compliant | RoHS-compliant |
| Process fundamentals | Identical | Identical |
| Market trend | Being phased out | Mainstream |
Related reading: HASL vs Lead-Free HASL: PCB Surface Finishes.
Process essentials and limitations:
| Item | HASL (leaded and lead-free) |
|---|---|
| Advantages | Low cost; good wettability and solderability; bright, high-strength joints with leaded HASL; stronger joints and RoHS compliance with lead-free HASL |
| Disadvantages | Relatively rough surface; copper can dissolve at high temperature; restrictions on very thick or thin boards; leaded HASL is not RoHS-compliant |
| Best for | General-purpose boards where cost matters; lead-free HASL for RoHS-compliant volume production |
| Avoid when | Fine-pitch components or BGAs; contact areas and tact switches; RoHS-compliant products (leaded HASL only) |
Immersion tin (ImSn, also called chemical tin or IMT) is a metal-type finish in which a pure tin layer is deposited directly on the copper surface by a chemical displacement reaction. Because almost all solder systems are tin-based, ImSn is compatible with any solder. Organic additives in the tin bath make the coating granular, which suppresses tin whiskers and tin migration and improves thermal stability and solderability. ImSn forms a flat Cu–Sn intermetallic compound (IMC) with the copper, giving excellent flatness and solderability for SMT, fine pitch and BGA. It is an environmentally friendly process intended to replace traditional Pb–Sn alloy electroplating, and it suits modern lead-free manufacturing.
Process essentials:
| Item | Immersion tin (ImSn) |
|---|---|
| Advantages | Excellent flatness for SMT, fine pitch, BGA and small components; medium cost and lead-free; compatible with all solders and with lamination; suits horizontal lines and fine geometries |
| Disadvantages | Sensitive to handling; short shelf life (about 6 months, tin-whisker risk); erodes solder mask and is not for peelable mask; electrical test needs soft probes; sensitive to strong acids and alkalis; long-term reliability and test convenience are inferior to ENIG and ENEPIG |
| Best for | Fine-pitch SMT, BGA, small components, lead-free assembly, and mass production that values flatness and environmental compliance |
| Avoid when | Long-term storage; contact parts and buttons; production lines with strict electrical-test fixture requirements; exposure to strong acids or alkalis |
Immersion silver (ImAg, IMS) sits between OSP and ENIG. It is easy to operate and fast, and it keeps good electrical performance and solderability in thermal, humid or contaminated environments, although the surface loses its luster. After the copper is cleaned and micro-etched, a silver layer is deposited by a galvanic displacement reaction. Without a nickel underlayer, its physical strength is lower than ENIG and it is more sensitive to creep corrosion.
Process essentials:
| Item | Immersion silver (ImAg) |
|---|---|
| Advantages | High solderability; flat surface; low cost and lead-free; suitable for aluminum wire bonding |
| Disadvantages | High storage requirements and easily contaminated; short assembly window after opening; electrical testing is difficult; weaker resistance to creep corrosion; excessive thickness or repeated deposition risks corrosion and open circuits |
| Best for | High flatness requirements, aluminum wire bonding, EMI shielding, fine lines and membrane switches |
| Avoid when | High-sulfur or high-contamination environments, long storage cycles, and lines that need convenient electrical testing |
ENIG has a Cu/Ni/Au three-layer structure. Electroless nickel (typically 3–5 µm) is deposited on the copper as a barrier and soldering layer, and a thin immersion gold layer (about 0.05–0.15 µm) on top prevents oxidation and keeps the surface solderable. During reflow the gold dissolves into the solder early, and the nickel layer forms the intermetallic compound (IMC) of the solder joint. ENIG offers high flatness and a long shelf life, and it suits plated through holes, multiple reflow cycles, high-density and fine-pitch assembly, keypads and COB.
Process essentials:
| Item | ENIG |
|---|---|
| Advantages | Flat surface; lead-free; suitable for plated through holes; long shelf life; suitable for multiple reflows and clean assembly; suits high-density and fine-pitch boards, keypads and COB |
| Disadvantages | Expensive and usually not reworkable; black pad or black nickel risk; possible RF signal loss; complex process; nickel layer may oxidize over time |
| Best for | High-density and fine-pitch boards, plated through holes, products that need long storage or multiple reflows, and assemblies with cleanliness requirements |
| Avoid when | Cost-sensitive or rework-sensitive designs; ultra-high-frequency, low-loss circuits (RF evaluation required); designs that need very high solder-joint strength |
Related reading:
>> HASL vs ENIG: An Ultimate Guide on Surface Finish.
>> ENIG PCB surface finish guide
ENEPIG has a Cu/Ni/Pd/Au four-layer structure. The palladium layer (0.1–0.5 µm) sits between the nickel and the gold. It protects the nickel from displacement corrosion during immersion gold, provides an excellent base for the gold layer, and significantly reduces the risk of black pad. The nickel layer is 3–6 µm and the gold layer is 0.02–0.1 µm. ENEPIG offers excellent flatness, solderability and compatibility, and it is commonly used for high-end package substrates, multi-cycle assembly and wire bonding.
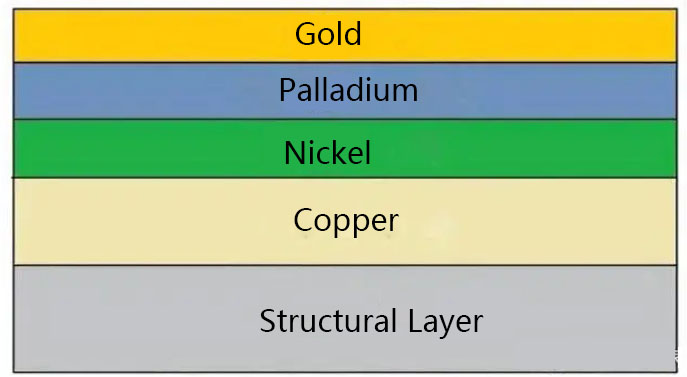
Process essentials:
| Item | ENEPIG |
|---|---|
| Advantages | Extremely flat; lead-free; suits multi-cycle assembly; excellent solder joints; supports wire bonding; significantly lower black pad risk; long shelf life (about 12 months or longer) |
| Disadvantages | Higher cost; reworkable but limited; strict handling and thickness-uniformity control |
| Best for | High-end packaging, SiP, wire bonding, and products with extremely high long-term reliability and flatness requirements |
| Avoid when | Mass production with strict cost constraints |
For a detailed comparison with ENIG, see ENIG vs ENEPIG, or read the ENEPIG PCB surface finish guide.
Electroplated nickel/gold deposits a nickel layer and then a gold layer on the copper by electrochemical methods. The nickel suppresses Cu–Au diffusion, and the gold provides conductivity and wear resistance. A 3–5 µm nickel layer is typically plated first, followed by 0.5–1.5 µm of gold, depending on the application. By the nature of the gold layer, it is divided into:
Process essentials:
Hard electrolytic gold over low-stress nickel provides excellent wear resistance. It suits edge-connector fingers, interconnect substrates, keyboard contacts and other high-wear areas.
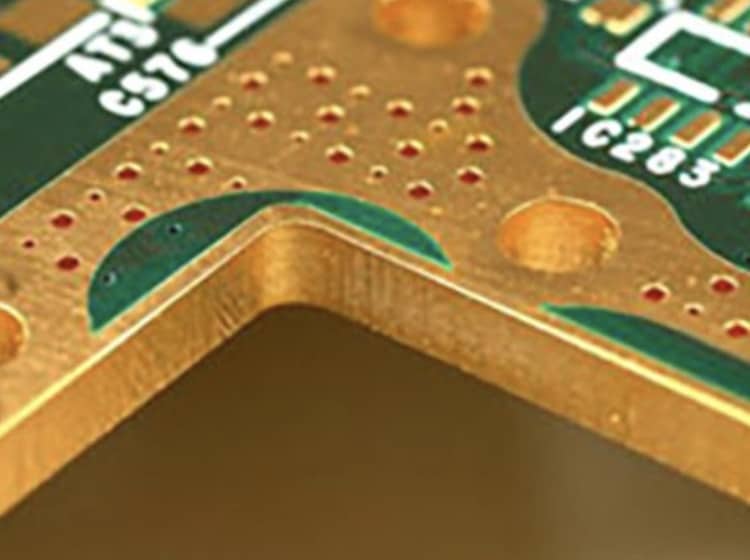
| Item | Hard gold |
|---|---|
| Advantages | Hard and wear-resistant; lead-free; long shelf life |
| Disadvantages | Very expensive; many steps (electroplating, bus bars, segmentation, masking); difficult to combine with other finishes; etch undercut can cause cracking or peeling; thick gold is not solderable; sidewalls outside the gold fingers are not fully encapsulated |
| Best for | Gold fingers, plug-in contacts, keyboard contacts, and highly reliable electrical contacts such as CPU sockets and memory modules |
| Avoid when | Solder pads, wire bonding, strict cost constraints, and non-contact areas that need full sidewall encapsulation |
Related reading: PCB Gold Fingers: Design & Manufacturing Guide.
Soft gold has high purity (99.9%), and its soldering and bonding performance is better than hard gold. It suits wire bonding and applications with higher requirements on solder-joint strength.
| Item | Soft gold |
|---|---|
| Advantages | Strong solderability and bondability; stronger solder joints |
| Disadvantages | High cost; wear resistance is lower than hard gold; also needs complex electroplating and masking |
| Best for | Wire bonding and designs where solderability comes first |
| Avoid when | High-wear contacts (use hard gold) and strict cost constraints |
OSP (also known as copper protector or Preflux) is a water-based organic molecule that selectively bonds with copper to form an organometallic layer about 0.10–0.60 µm thick. It protects against oxidation and sulfidation at room temperature. During reflow, flux quickly removes the layer, and the bare copper immediately combines with solder to form a strong joint. OSP only provides short-term solderability protection, but it is environmentally friendly, low-cost and flat, which makes it well suited to fine-pitch SMT.
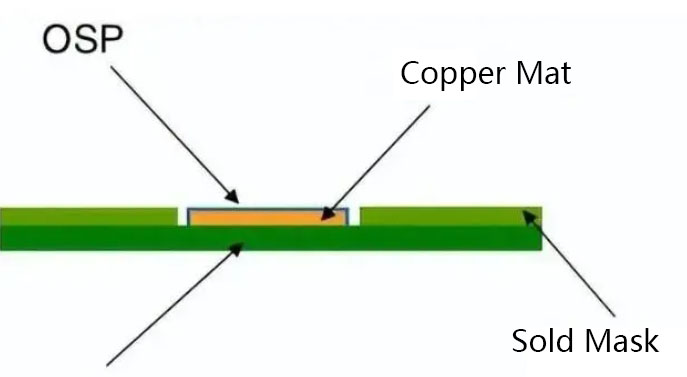
Process essentials:
| Item | OSP |
|---|---|
| Advantages | Flat; simple process; environmentally friendly; low cost; supports lead-free and SMT; reworkable; suits horizontal lines |
| Disadvantages | Thickness cannot be measured easily; not suitable for plated through holes; short shelf life; may cause ICT problems; copper may be exposed during assembly; sensitive to handling; limited rework; not suitable for press-fit or wire insertion; inconvenient for visual and electrical test |
| Best for | Cost-sensitive products, fine-pitch SMT, and products with high flatness requirements and a fast assembly cadence |
| Avoid when | Long-term storage; wave or selective wave soldering; scenarios that need plated-through-hole or ICT friendliness |
Related reading: What Is PCB OSP Surface Finish?
A single surface finish rarely covers every functional, cost and environmental need, so hybrid surface finishing, which uses two or more processes in different areas of the same PCB, has become common. It balances high reliability in critical zones with lower cost elsewhere. Typical combinations are ENIG + OSP, electroplated Ni/Au + ENIG, electroplated Ni/Au + HASL, ENIG + HASL, and lead-free HASL + gold fingers (electroplated hard gold).
| Option | Applicable | Limitations and notes |
|---|---|---|
| ENIG + OSP | High flatness and long-term reliability on critical pads, lower cost elsewhere | Complex process sequence; high requirements for regional masking |
| Electroplated Ni/Au + ENIG | Balances contact wear resistance and soldering flatness | Complex electroplating fixtures, bus bars and masking; high cost |
| Electroplated Ni/Au + HASL | Wear resistance in contact areas, low cost in non-critical areas | Differences in surface height and solder accumulation need evaluation |
| ENIG + HASL | Flatness in fine-pitch areas, economy in conventional areas | Failure modes such as RF loss, black pad and thermal shock need verification |
| Lead-free HASL + gold fingers | Wear resistance for plug-in contacts, economy for the rest of the board | Hard-gold thickness and boundary control are required in the gold-finger area |
Every finish starts with surface conditioning, which means cleaning and micro-etching the copper so the coating bonds evenly. The steps after that differ by finish.
| Finish | Typical process steps | Key control points |
|---|---|---|
| HASL | Clean and micro-etch, apply flux, dip in molten solder, level with hot-air knives, cool and clean | Solder temperature and air-knife settings set coating thickness and flatness |
| Immersion tin | Clean, micro-etch, pre-dip, chemical displacement tin deposition, rinse and dry | Bath additives; avoid strong acids and alkalis after deposition |
| Immersion silver | Clean, micro-etch, galvanic displacement silver deposition, thorough rinse and dry | Silver thickness (keep under 0.5 µm) and thorough rinsing and drying |
| ENIG | Cleaning, etching, activation, electroless nickel, immersion gold, residue cleaning | Nickel chemistry control to avoid black pad; gold at or below 0.3 µm |
| ENEPIG | Clean, micro-etch, activation, electroless nickel, electroless palladium, immersion gold | Palladium layer protects the nickel during gold deposition; thickness uniformity |
| Electroplated Ni/Au | Electroplate nickel, then electroplate hard or soft gold, using bus bars and masking | Current density, time and solution composition set thickness and hardness |
| OSP | Degreasing, micro-etching, acid wash, pure-water rinse, organic coating, rinse | Coating thickness is hard to verify online, and too thick a film affects soldering |
| Finish | Layer structure | Typical thickness | Notes |
|---|---|---|---|
| ENIG | Cu / Ni / Au | Ni about 3–5 µm; Au about 0.05–0.15 µm | Keep gold at or below 0.3 µm; gold above 3% of the joint makes it brittle |
| ENEPIG | Cu / Ni / Pd / Au | Ni 3–6 µm; Pd 0.1–0.5 µm; Au 0.02–0.1 µm | Thin, soft gold needs mechanical protection |
| Electroplated Ni/Au | Cu / Ni / Au | Ni about 3–5 µm; Au 0.5–1.5 µm, depending on the application | Thickness and hardness are set by plating conditions |
| Hard gold (contacts) | Cu / Ni / hard Au | Au 50–100 µin (military) or 25–50 µin (consumer), over a Ni base thicker than 100 µin | Gold above about 17.8 µin reduces solderability |
| Immersion silver | Cu / Ag | Thin displacement layer; keep under 0.5 µm | Excess thickness risks galvanic corrosion and open circuits |
| OSP | Cu / organic film | About 0.10–0.60 µm | Thickness is difficult to measure online |
Unit conversion: 1 µin (microinch) = 0.0254 µm. Thickness targets vary with the IPC class and the customer specification. IPC publishes dedicated specifications for several finishes, including IPC-4552 (ENIG), IPC-4553 (immersion silver), IPC-4554 (immersion tin) and IPC-4556 (ENEPIG).
Finish selection directly affects process yield, rework, field failure rates, testability, scrap rates and cost. To get a high-quality, high-performance product, weigh every assembly consideration when you select the finish. The table lists the main criteria and the finishes that fit each one.
| What matters | Choose | Be careful with | Why |
|---|---|---|---|
| Pad flatness (fine pitch, BGA) | ENIG, ENEPIG, OSP, immersion tin | HASL | These finishes form thin, uniform layers, while HASL leaves a rougher surface |
| Solderability and wetting | HASL, ENIG, ENEPIG | OSP after long storage or repeated reflow | The OSP film ages and has limited tolerance for reflow and rework |
| Wire bonding | Gold wire: ENEPIG, soft gold. Aluminum wire: ENEPIG, immersion silver | Hard gold | Hard gold is not suitable for wire bonding |
| Storage and handling | ENIG, ENEPIG, hard gold | OSP, immersion tin, immersion silver | These have short shelf lives or are sensitive to handling and contamination |
| Soldering and rework cycles | ENIG, ENEPIG, HASL | OSP (about 2 reworks), immersion tin | The thin organic film and tin layer tolerate few thermal cycles |
| RoHS compliance | Lead-free HASL, immersion tin, immersion silver, ENIG, ENEPIG, OSP, gold | Leaded HASL | Finishes that use lead are not RoHS-compliant |
| Contacts and wear | Hard gold | HASL, OSP, immersion tin on contact areas | Hard gold resists repeated insertion; the others are not designed for contacts |
| RF and high-frequency signals | Immersion silver, gold | ENIG | The nickel layer in ENIG may add RF signal loss, so evaluate it for low-loss designs |
| Cost | HASL, OSP | ENEPIG, electroplated gold | Multilayer and electroplated finishes cost more |
The comparison chart below shows which attributes each surface finish does and does not have. Use it with the table above to pick the right option for your product requirements.
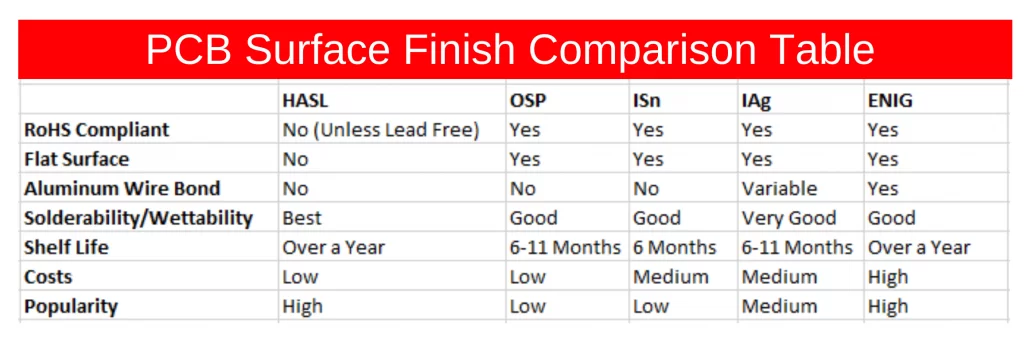
These are the finishes commonly used for specific board types and applications. Your assembly process and storage plan can change the final choice, so confirm the finish during design review.
| Board or application | Commonly used finishes | What to check |
|---|---|---|
| Consumer and general-purpose boards | Lead-free HASL, OSP | Cost, RoHS compliance and how soon boards are assembled |
| High-precision, fine-pitch and BGA boards (see HDI PCBs) | ENIG, ENEPIG, OSP, immersion tin | Pad flatness, minimum pad size and storage time |
| LED PCBs | Lead-free HASL, OSP, ENIG | Assembly temperature profile and pad flatness for small LED packages |
| Camera modules and compact boards (see flex PCBs and rigid-flex PCBs) | ENIG, ENEPIG | Small pads, bending stress and any wire bonding |
| Heavy copper power boards | Lead-free HASL, ENIG | Pad flatness needs of the controllers and sensors, and finish coverage over thick copper; confirm in design review |
| Ceramic PCBs | ENIG, ENEPIG, electroplated Ni/Au (soft gold) | Wire bonding or die attach requirements |
| High-frequency and RF boards | Immersion silver, gold | Signal loss; ENIG’s nickel layer needs RF evaluation; keep silver boards sealed |
| Connectors, edge contacts and gold fingers | Hard gold on the contact area, with ENIG, HASL or OSP elsewhere | Gold thickness, bevel and boundary control; see the gold fingers guide |
| Automotive, medical and industrial high-reliability boards (see automotive and medical PCBs) | ENIG, ENEPIG | Long storage, multiple reflows and black pad control |
When choosing a surface finish, fitness for purpose matters more than reputation. Your component pitch, assembly process (reflow, wave or selective soldering), long-term storage needs, contact wear resistance, RF loss tolerance and cost targets all drive the decision. NextPCB provides finish selection and manufacturing collaboration so design, manufacturing and assembly start from the same process window.
| Quote page | Surface finishes |
|---|---|
| Standard PCB quote | HASL, lead-free HASL, ENIG, OSP |
| Advanced PCB quote | Immersion silver, immersion tin, ENEPIG, hard gold and gold fingers, plus the standard finishes on advanced boards such as HDI, rigid-flex and high-frequency |
See the full list with specifications on the PCB surface finish options page, and check board limits in the standard PCB capabilities and advanced PCB capabilities.
Full range of finishes: HASL (leaded and lead-free), ImSn (immersion tin), ImAg (immersion silver), ENIG, ENEPIG, electroplated Ni/Au (hard gold and soft gold), OSP, and selective or partitioned hybrid finishes such as “gold finger electroplating plus ENIG, HASL or OSP on the other areas.”
Send us your project key points or files, and let NextPCB’s engineering team match the right surface finish to the right manufacturing window, so yield, reliability and cost all work out together.
A PCB surface finish is a thin metallic or organic coating on the exposed copper pads of a printed circuit board. It protects the copper from oxidation and provides a solderable surface for component assembly.
The main types are HASL (leaded and lead-free), immersion tin, immersion silver, ENIG, ENEPIG, electroplated nickel/gold (hard gold and soft gold) and OSP. Hybrid finishes combine two or more of them on the same board.
No single finish is best for every board. Lead-free HASL suits cost-sensitive general-purpose boards, ENIG and ENEPIG suit fine-pitch and high-reliability boards, OSP suits flat pads with fast assembly, and hard gold suits contacts and gold fingers. Choose by component pitch, assembly process, storage time, wear and RF requirements, and cost.
ENIG deposits a flat nickel and gold layer that stores well and survives multiple reflows, which suits fine-pitch parts and BGAs. HASL coats the pads with molten solder and levels it with hot air, which costs less but leaves a rougher surface. See the HASL vs ENIG guide for a full comparison.
Leaded HASL uses a tin-lead (Sn–Pb) alloy that melts at about 183 °C and is not RoHS-compliant. Lead-free HASL uses a tin-silver-copper (SAC) alloy that melts at about 217 °C, gives stronger solder joints and is RoHS-compliant. The process is the same; only the alloy differs.
Every finish in this guide is lead-free except leaded HASL: lead-free HASL, immersion tin, immersion silver, ENIG, ENEPIG, electroplated nickel/gold and OSP. For RoHS-compliant products, avoid any finish that uses lead.
ENIG and ENEPIG are the usual choices because they give very flat pads and a long shelf life. OSP and immersion tin also give flat pads, but they have shorter shelf lives and limited tolerance for rework. HASL is not recommended for fine pitch because of its rougher surface.
ENEPIG and electroplated soft gold are the preferred choices for gold wire bonding. ENEPIG and immersion silver also suit aluminum wire bonding. Hard gold is not suitable for wire bonding.
ENIG, ENEPIG and hard gold have long shelf lives, and ENEPIG typically lasts about 12 months or longer under good control. HASL also stores well. Immersion tin is generally limited to about 6 months because of tin-whisker risk, and OSP and immersion silver have short assembly windows after the package is opened. Keep boards sealed and assemble them promptly.
Solderability is tested to IPC J-STD-003 using methods such as the edge dip (dip and look) test, the wetting balance test and the surface mount simulation test, run on finished boards or test coupons. Coating thickness measurement by XRF and microsection analysis complement these tests.
Black pad is an ENIG defect in which the nickel surface corrodes during immersion gold deposition, leaving a brittle layer that wets poorly and forms weak solder joints. It is controlled through strict process control of the electroless nickel and immersion gold chemistry, and the palladium layer in ENEPIG significantly reduces the risk. For causes, detection and prevention, read our black pad guide.
Still, need help? Contact Us: support@nextpcb.com
Need a PCB or PCBA quote? Quote now


 PCB Assembly